
Understand
Why it makes a good part
Studies that show how the process behaves.
Injection Moulding process knowledge
Anyone can make a good part. The work is making every part good — consistently, efficiently, and for the right reasons. PolyTakt helps technicians, engineers, and managers understand the process, optimise it, and hand those decisions on.
Available worldwide on Google Play and the App Store. No account required for core tools; works offline once installed.
Cloud sync, custom materials, and the scientific suite on your phone.
Explore Pro →A shared company library and user licences in packs of five — from €12.50/licence/month, billed annually.
View Teams →Evidence-led articles from the moulding floor — written for technicians, engineers, and quality teams.
Visit the blog →From material to measured part
Understand
Studies that show how the process behaves.
Optimise
Repeatability, robustness, and cycle time, once the process is understood.
Verify
A visual check and a dimensional check of the part.
Shop-floor tools in one place
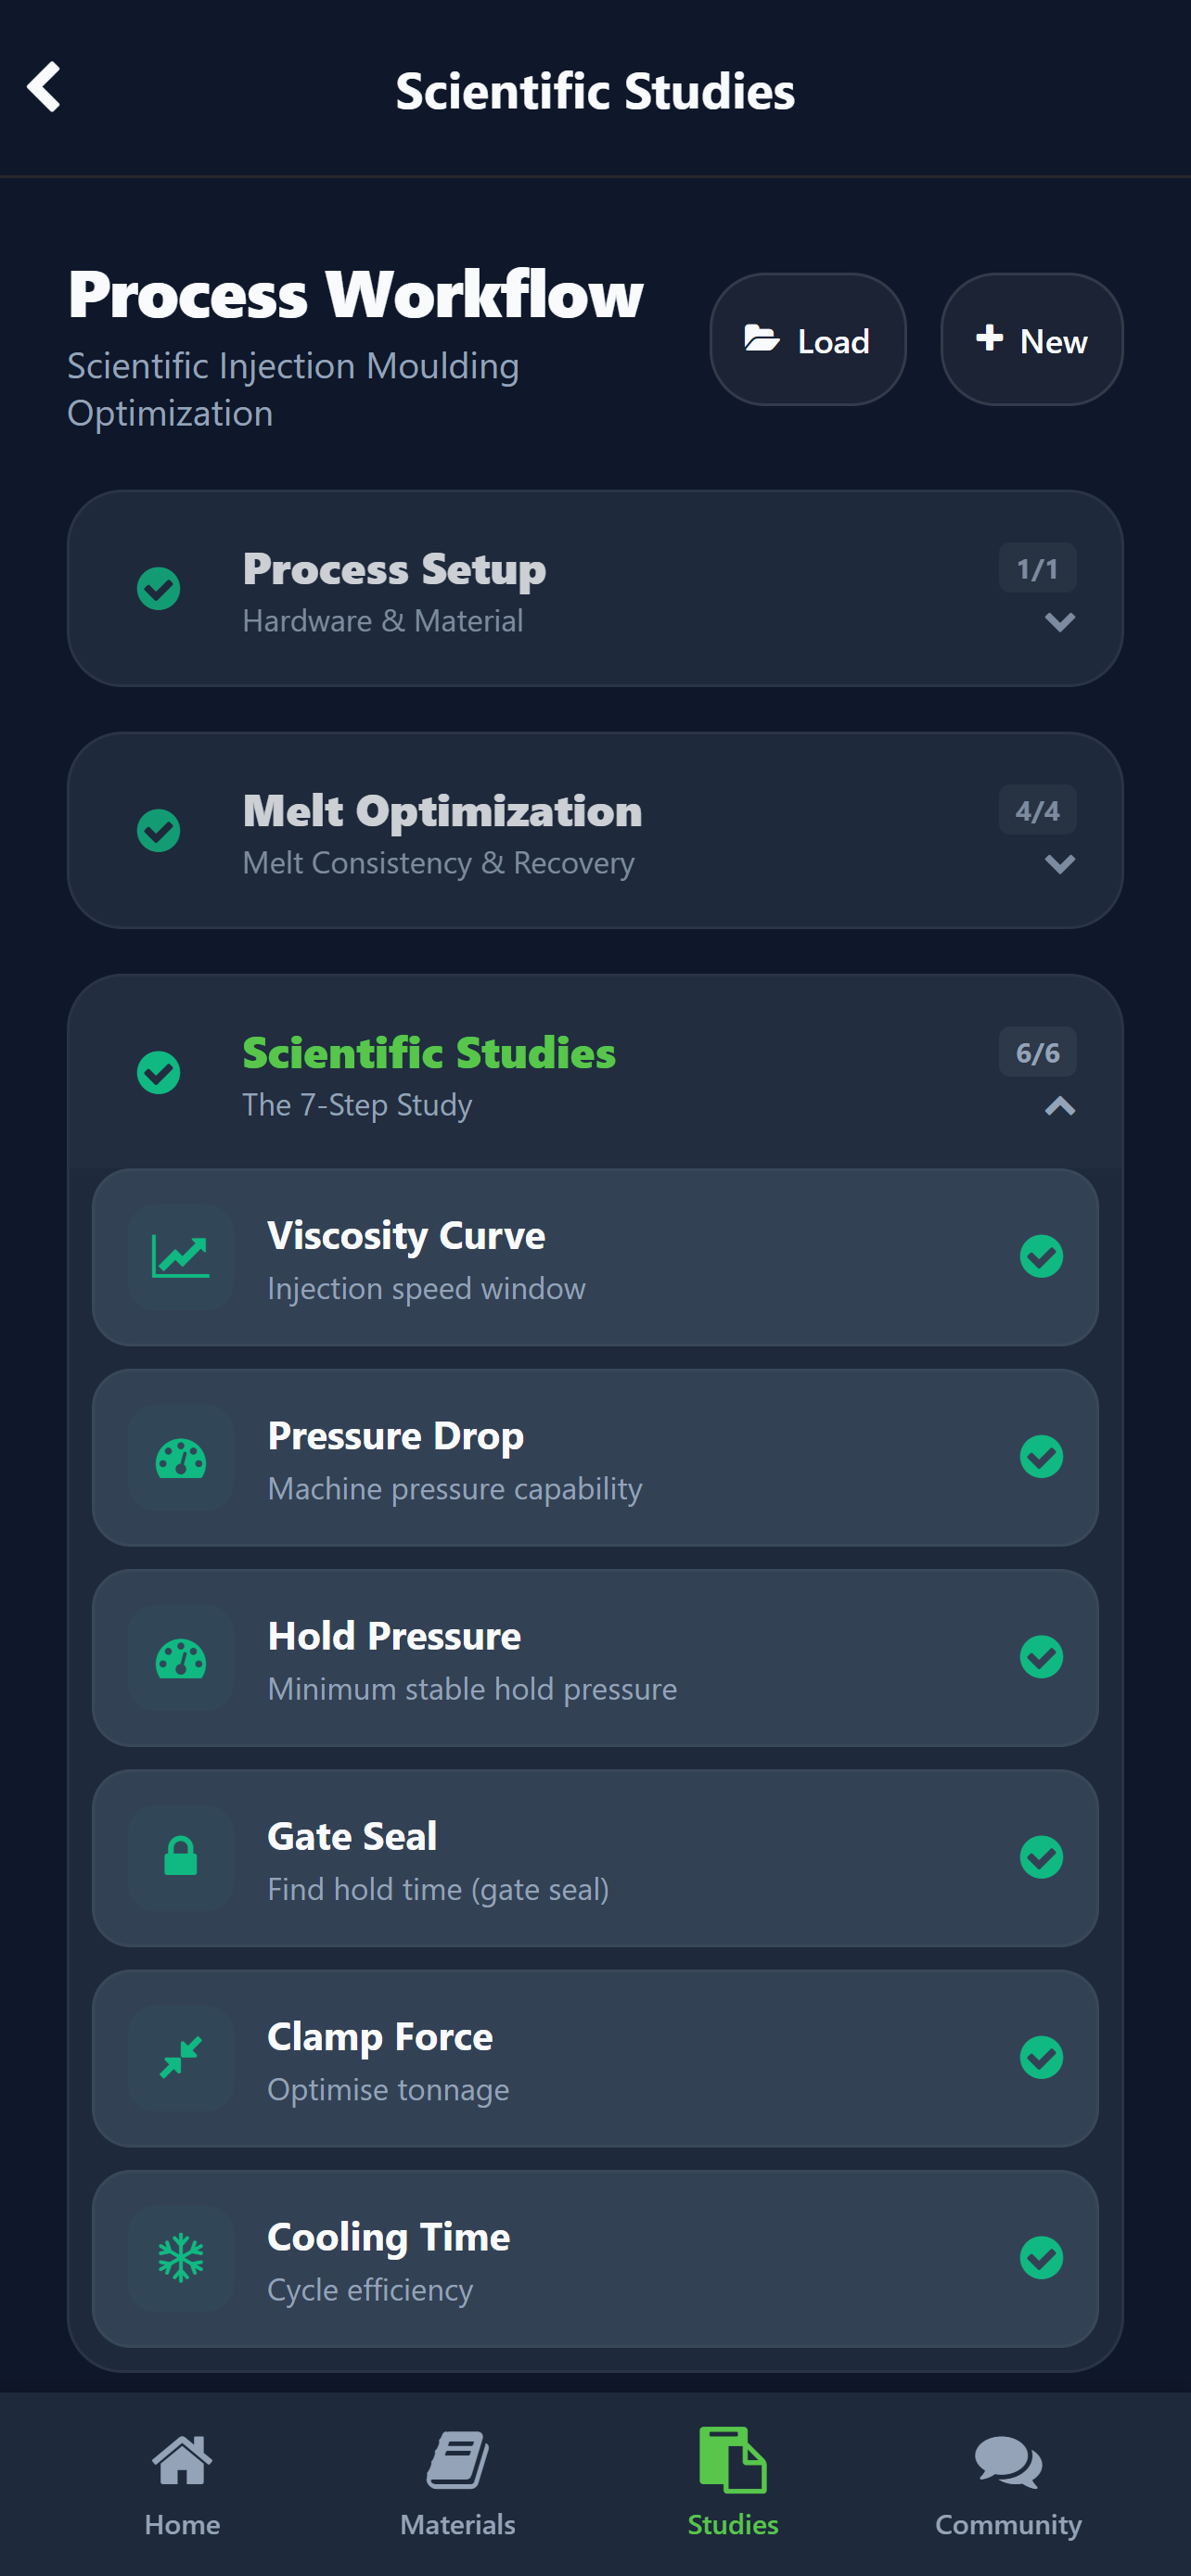
Scientific studies, step by step
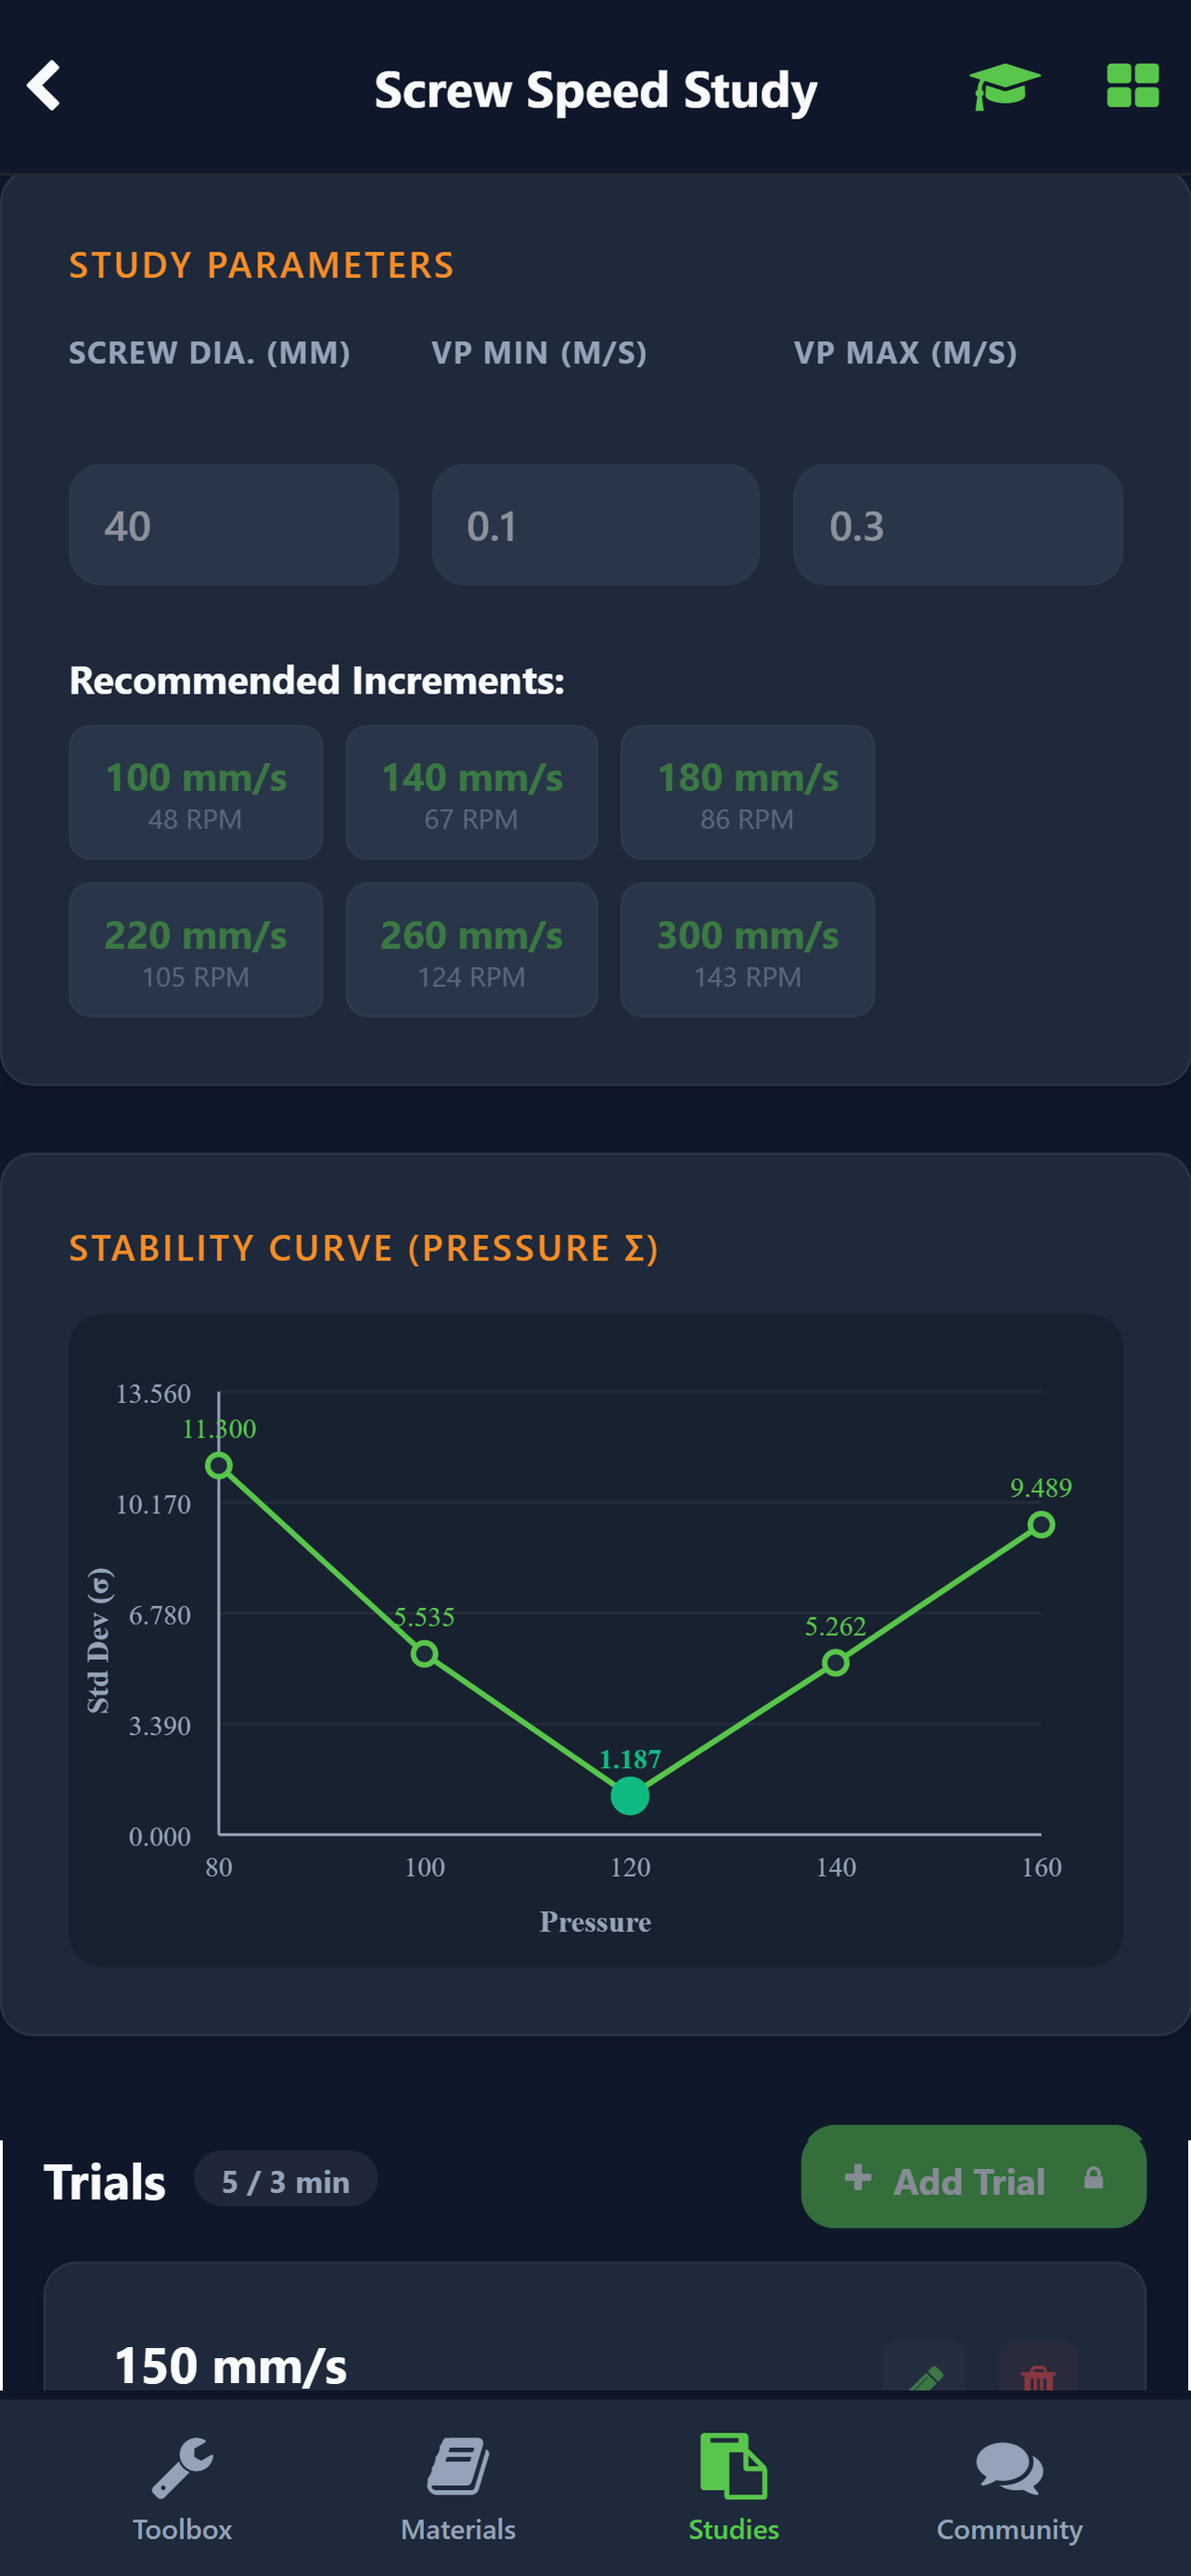
A screw-speed study, with the curve on screen
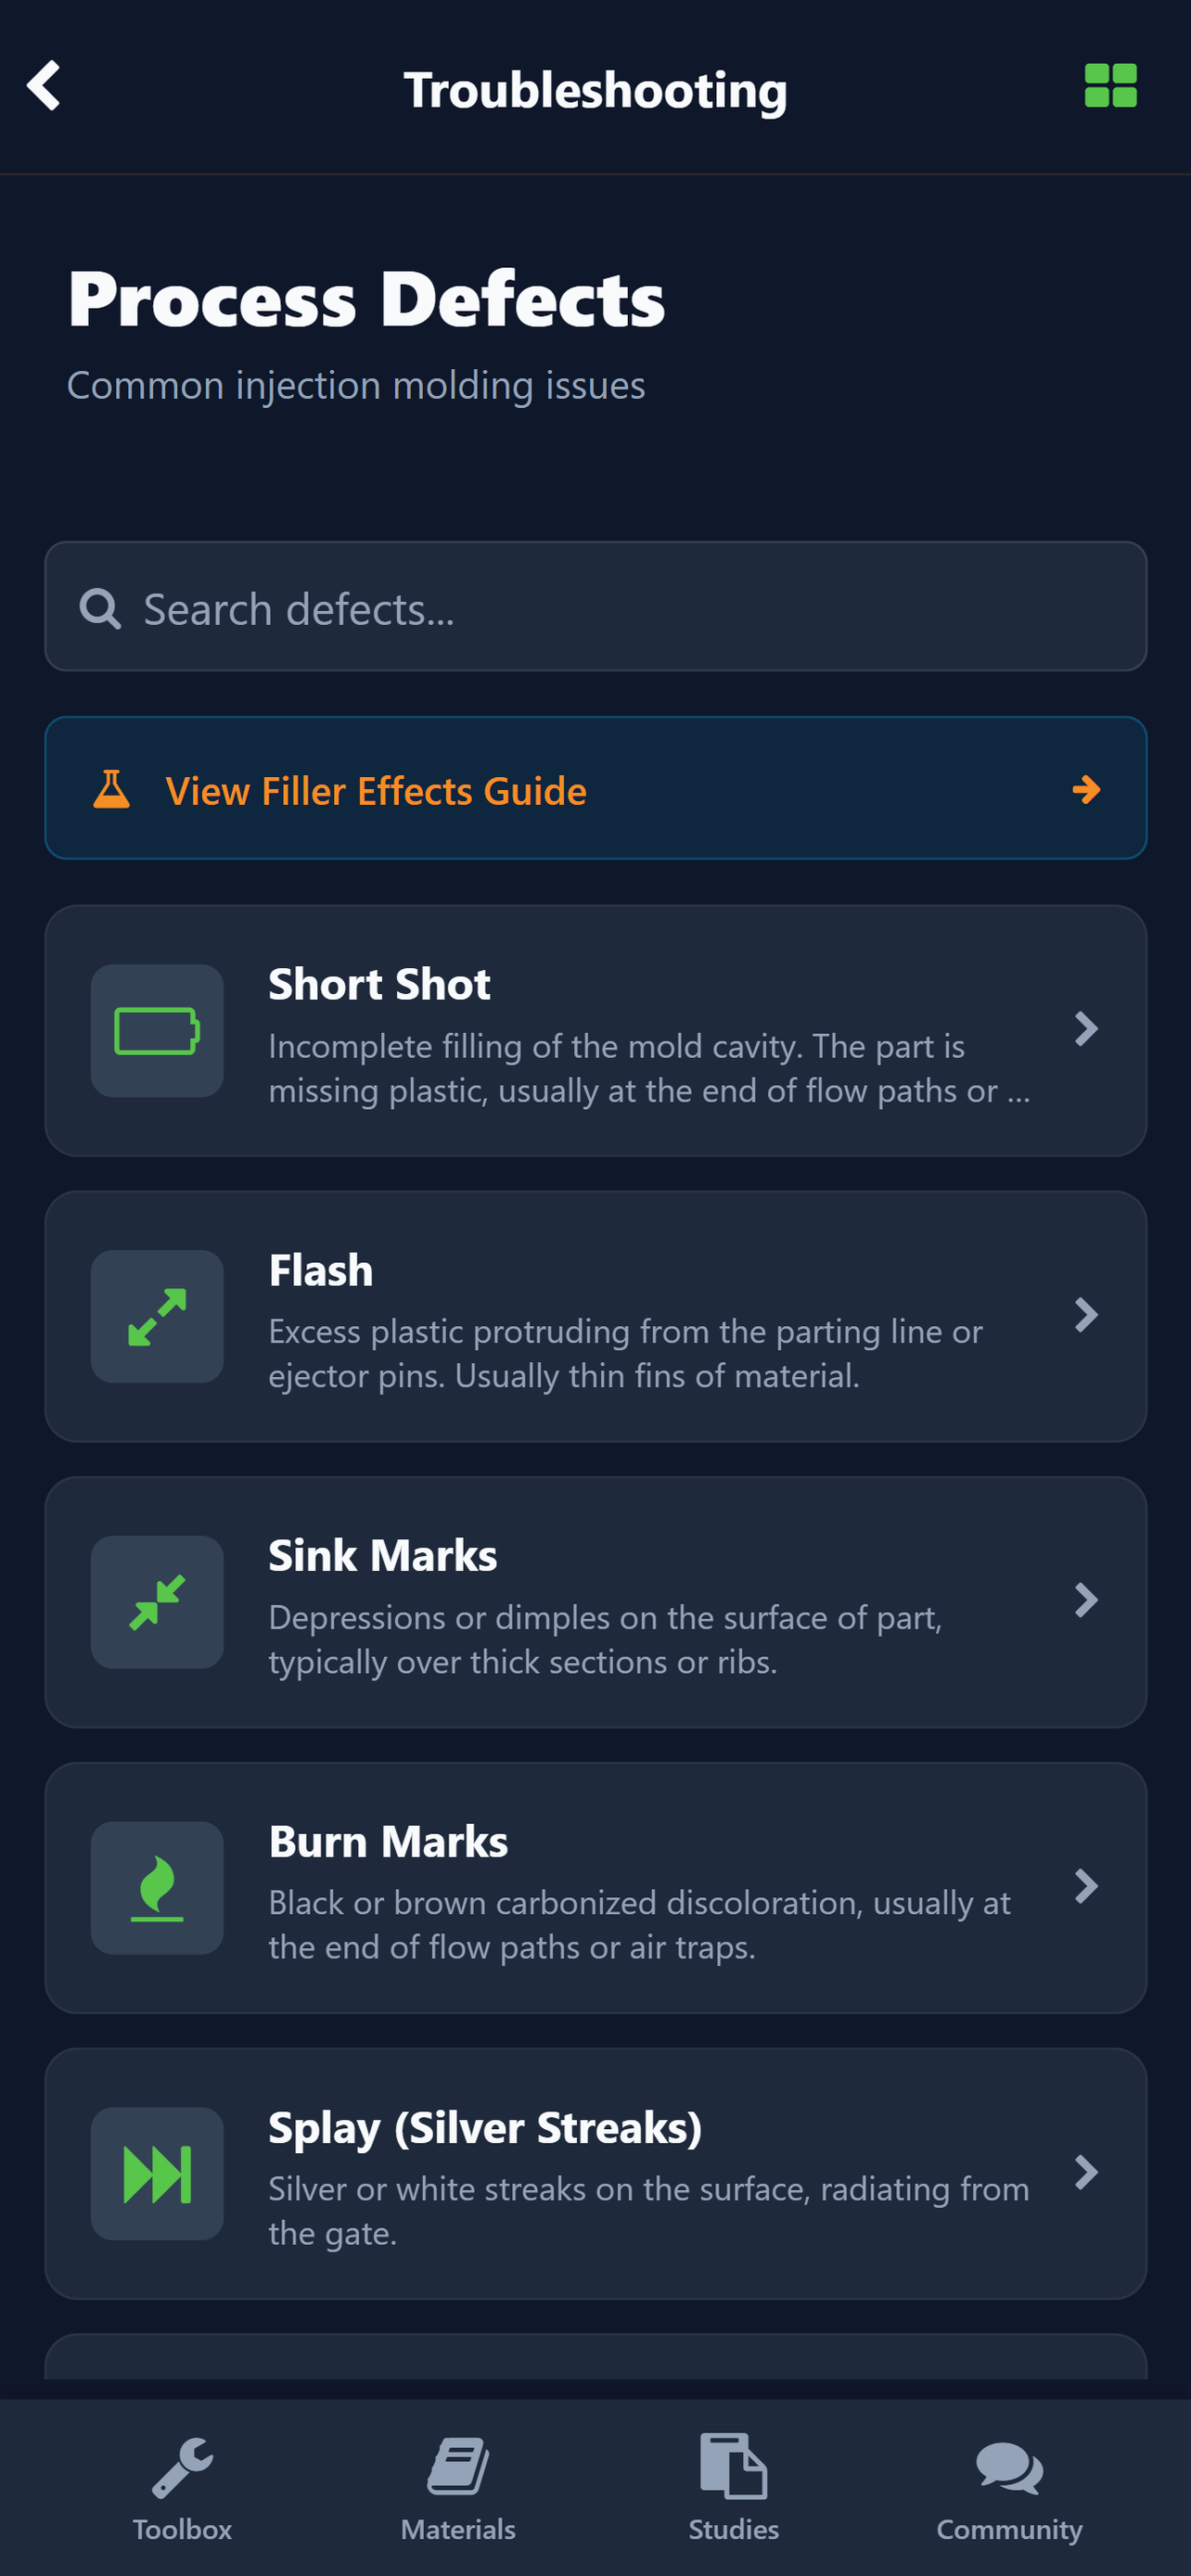
Troubleshooting from the defect in front of you
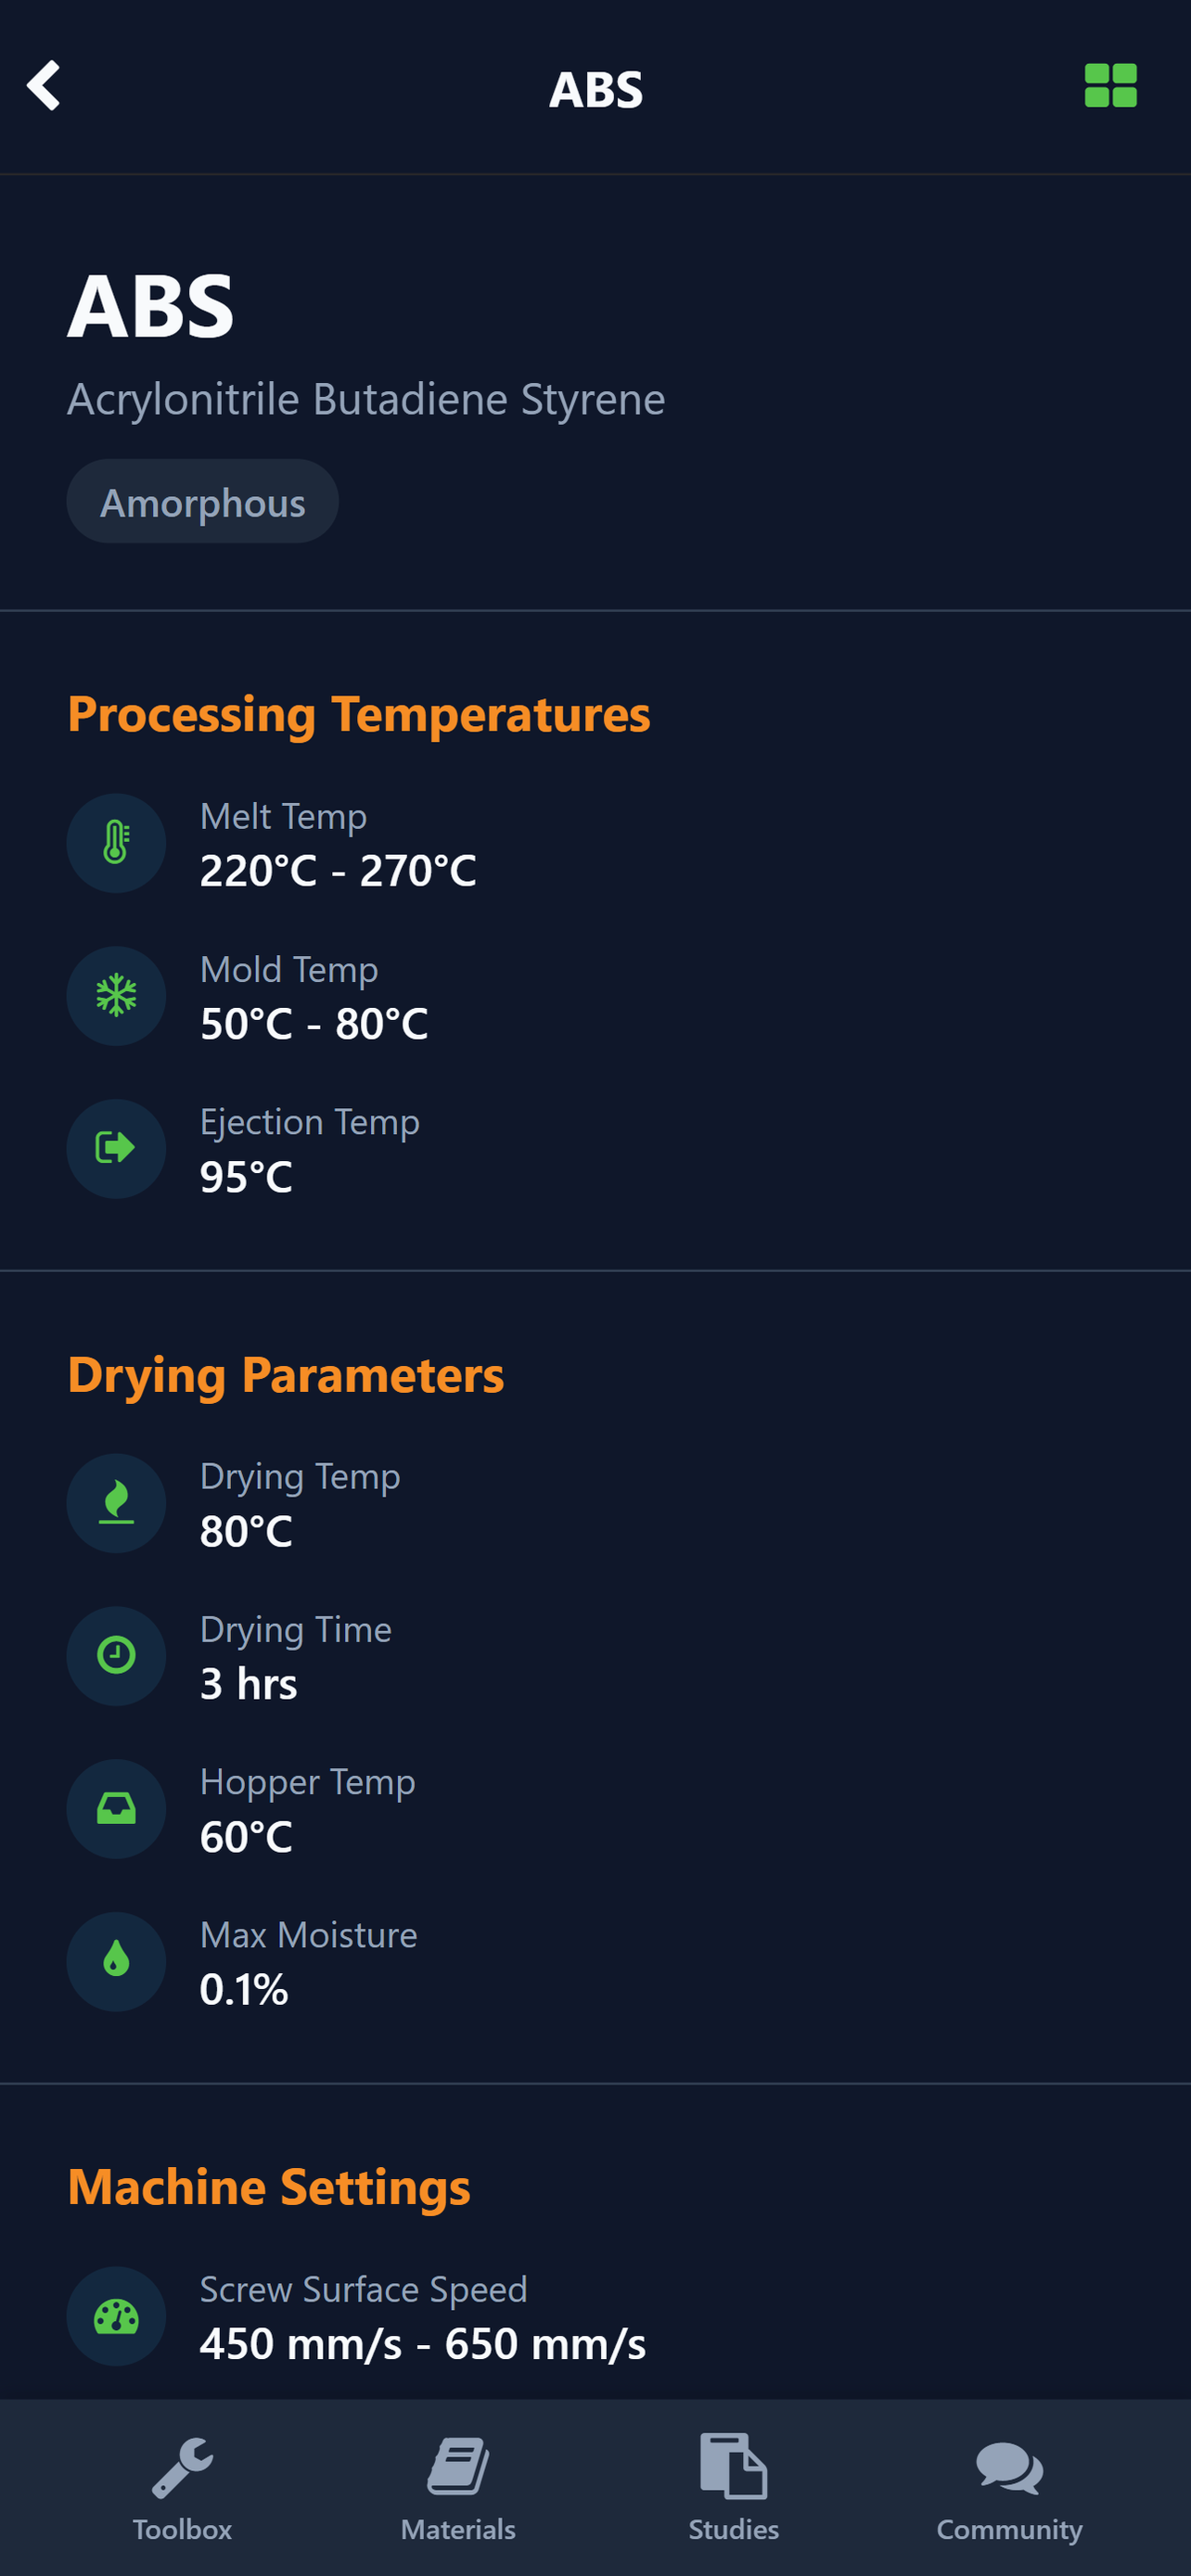
Processing data for the material on the job
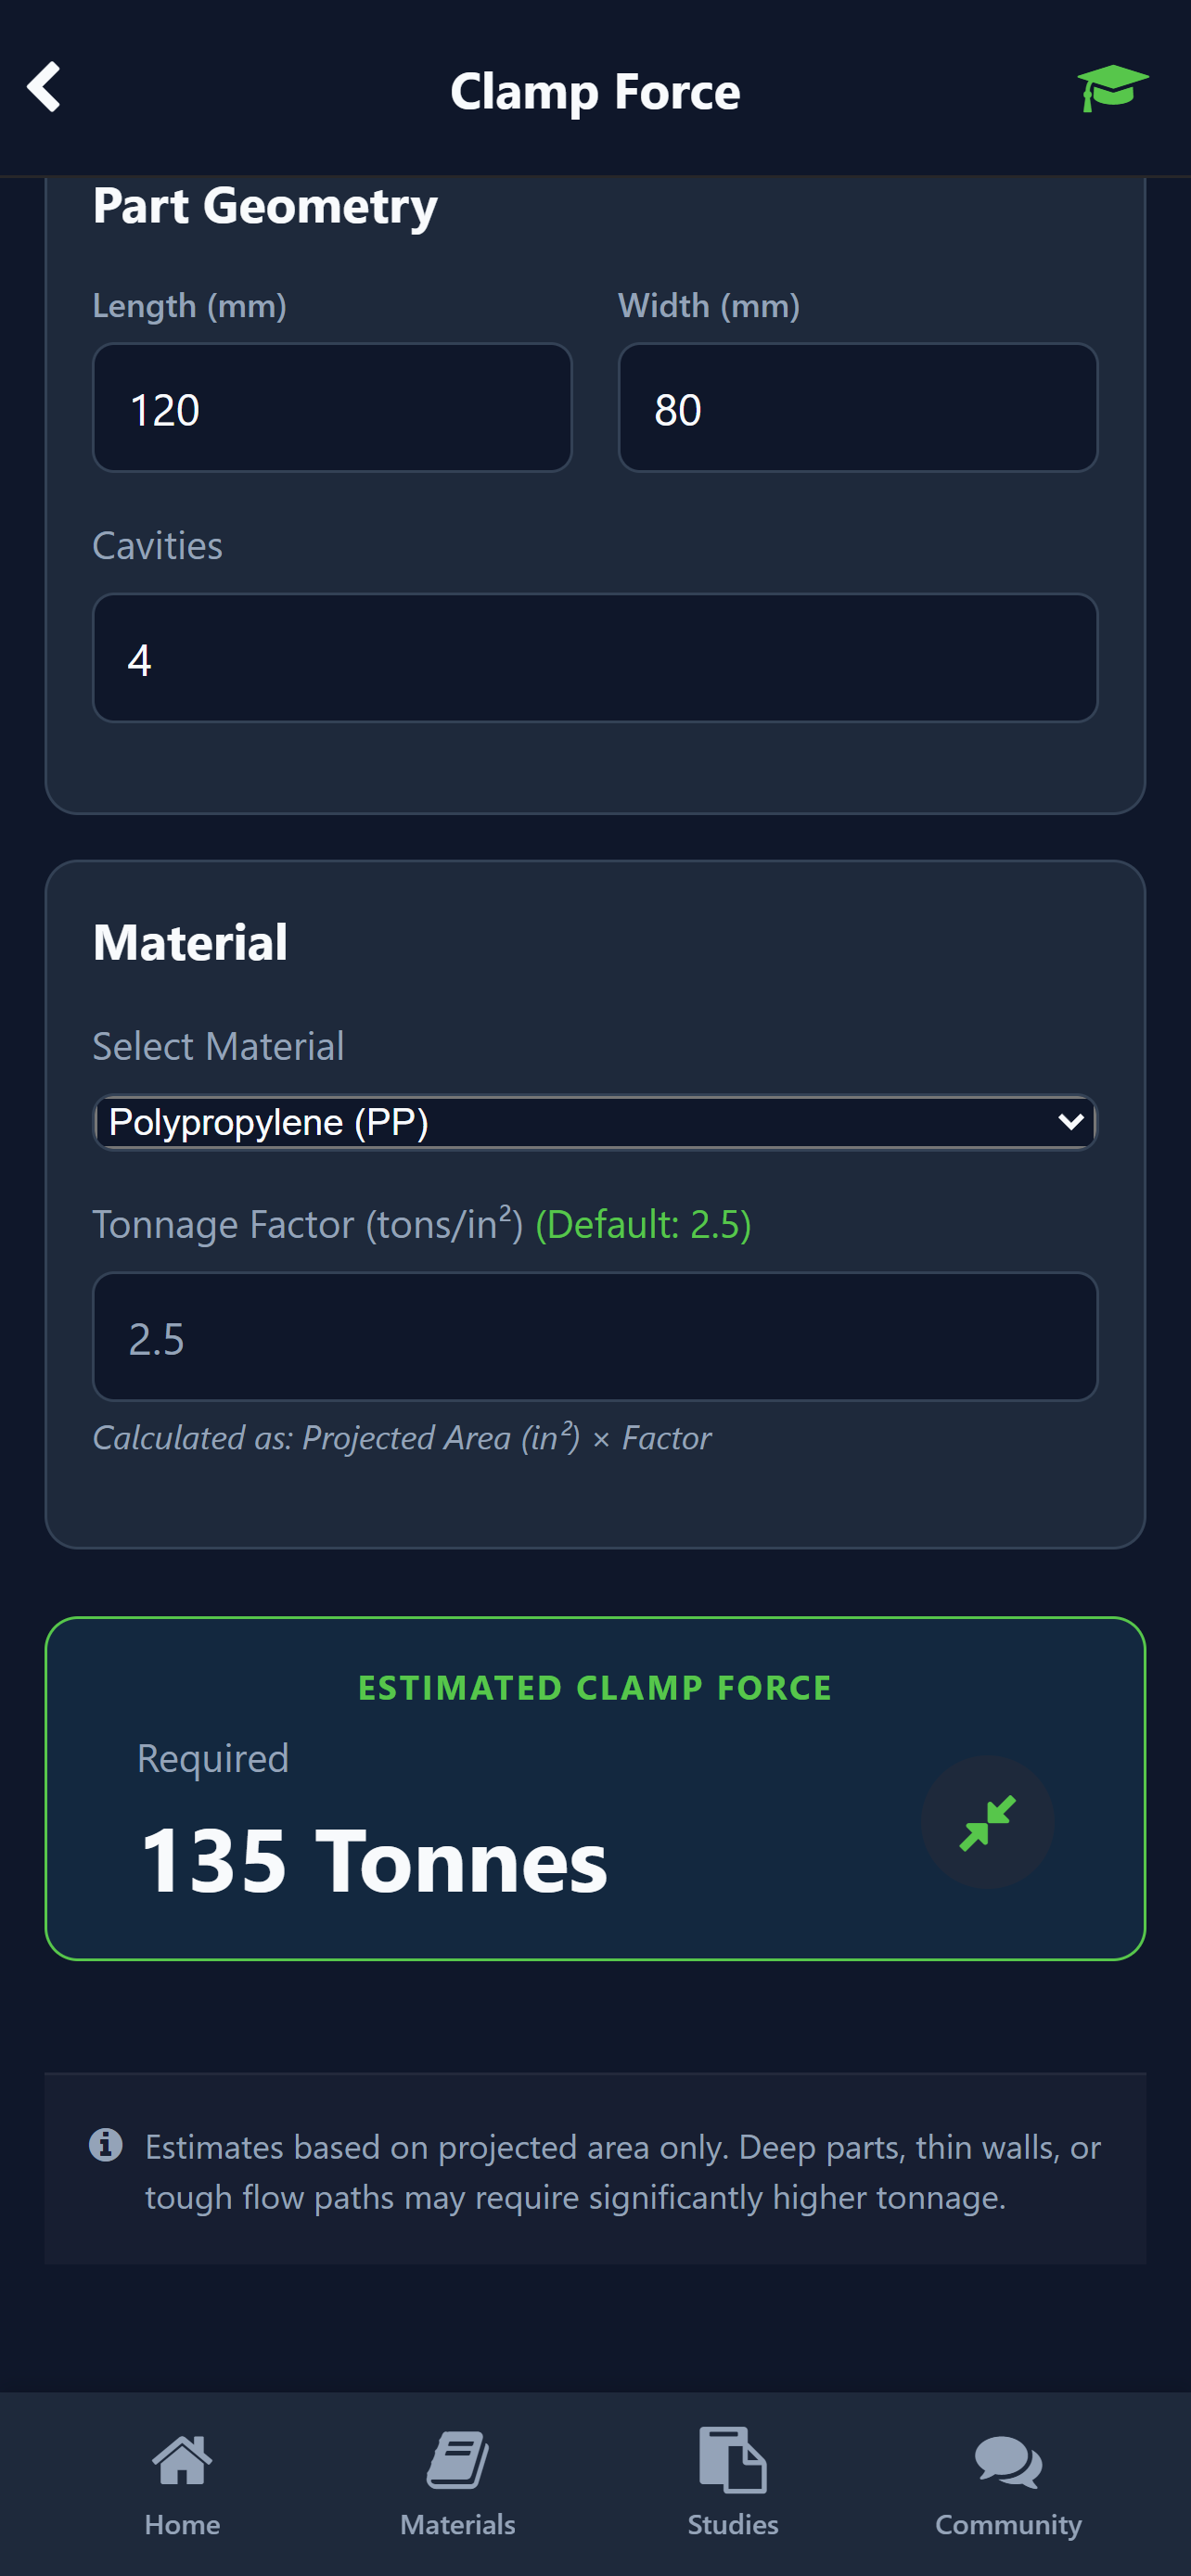
Clamp force from the part you are running
Now on Android and iOS
Teams Mobile
User licences in packs of five. The team shares the same machines, materials, and moulds.
Practical knowledge
The PolyTakt blog publishes practical process guidance and industry perspectives — written for technicians, engineers, and quality teams.
Process development
A process window is the range where the part is still acceptable, and it is unfinished until you also record where production will run inside it. This article covers which settings the earlier studies already fixed, how to map second-stage pressure, cooling time, and the temperature the material uses, and how to choose a working point without defaulting to the middle of the range.
Process development
V/P transfer is where fill ends and pack begins. A first stage of 95–98% by volume is widely taught, and it does not always mean the same appearance. This article sets out both readings, how to see them on fill-only shots, and how to document the job you have given pack.
Process development
A gate seal study (also called a gate freeze study) finds when shot weight stabilises — when the gate has sealed and further second-stage time adds nothing. This article covers the default single-phase Hold Time method, an optional dual-phase Pack and Hold protocol for thick-walled parts, gate-type considerations, what to do when weight never plateaus, and how results support production and validated moulding.